


In today’s fast-paced global market, effective warehousing and materials management are vital for successful supply chains. However, traditional methods often encounter challenges. Manual data input often results in mistakes, which can create major inconsistencies in inventory records. The ongoing struggle for quick and accurate item location results in higher labor costs.
Furthermore, issues like theft, loss, and damage can severely impact profitability and customer satisfaction. These operational challenges hinder productivity and limit a company’s growth and competitiveness. RFID (Radio Frequency Identification) technology offers a groundbreaking solution for enhancing inventory and materials management.
Understanding Warehousing and Materials Management
Effective warehousing and materials management are pivotal for any organization dealing with physical goods. While often used interchangeably, these terms represent distinct yet highly interconnected sets of activities crucial for a seamless supply chain.
What is Warehousing Management?
Warehouse management involves the planning, coordination, and execution of daily tasks to ensure efficient operation within a warehouse. This includes the systems and methodologies used to control inventory, streamline workflows, and optimize resources. Its primary goal is to manage the flow and storage of products while overseeing shipping, receiving, storage, and order picking. Effective warehouse management ensures secure storage, easy access, and efficient transportation of products to meet customer demands. This involves optimizing space, managing workforce resources, maintaining equipment, and protecting inventory. Modern warehouse management also focuses on leveraging technology to improve accuracy and speed, reducing reliance on manual tasks that can cause errors. The ultimate aim is to create a well-organized and agile environment that supports the broader supply chain objectives.
What is Materials Management?
Materials management is essential in supply chain operations, involving the planning and oversight of material flow from acquisition to distribution. Its main goal is to ensure the right quality and quantity of materials are available at the right time and place, while minimizing costs. Effective materials management helps reduce inventory costs and ensures timely production and order fulfillment, enhancing resource efficiency and profitability.
What are RFID Tags?
RFID tags are essential for efficient smart warehousing and inventory management. These small devices, made up of a microchip and antenna, store key data like item IDs. They communicate with RFID readers using radio-frequency signals, enabling scanning without a direct line of sight, unlike barcodes. This allows for reading from several meters away and through non-metallic surfaces, which speeds up data capture and reduces manual effort. The versatility and advanced features of RFID tags are crucial for automating data collection and improving supply chain visibility.
Why Implement RFID Tags for Efficient Warehousing and Materials Management?
Maintain Accurate Inventory
One of the most significant advantages of inventory tracking with RFID is the dramatic improvement in inventory accuracy. Manual counting and barcode scanning are prone to human error, leading to discrepancies between recorded stock and actual physical stock. RFID tags enable fast and accurate scanning of large quantities of items simultaneously, without the need for a direct line of sight. This means entire pallets or shelves of goods can be inventoried in seconds, drastically reducing the time and labor involved in stock-taking. With near real-time updates to inventory records, businesses can trust their data, minimize stockouts, reduce overstocking, and improve order fulfillment rates. This accuracy is fundamental to efficient warehousing and materials management.
Improve Warehousing Efficiency
RFID technology significantly enhances warehouse automation and overall operational efficiency. Tasks such as receiving, put-away, picking, and shipping become faster and less labor-intensive. For instance, upon arrival, goods tagged with RFID can be automatically identified and registered into the warehouse management system (WMS). This reduces search times, minimizes mis-picks, and accelerates the entire order processing cycle. The ability to quickly locate and process items contributes directly to a more agile and responsive warehouse environment, a key component of smart warehousing.
Real-time Visibility of Inventory and Materials
Real-time inventory visibility revolutionizes warehousing and materials management. By utilizing RFID systems, businesses can continuously track tagged items throughout the supply chain, from production to delivery. Implementing RFID readers strategically across a warehouse or logistics network allows for automatic capture of goods’ locations and statuses. This ongoing data flow provides an immediate overview of inventory levels and movements, empowering managers to make informed decisions, swiftly identify bottlenecks, and adapt to fluctuating demands. Such transparency is essential for effective RFID logistics and optimizing the entire supply chain process.
Higher Material Utilization and Faster Turnover
Improved visibility and precision through RFID directly enhance material utilization and accelerate inventory turnover. By having a clear understanding of available materials and their locations, companies can optimize their usage and minimize waste. For example, in manufacturing, RFID can monitor work-in-progress (WIP) items, ensuring a seamless flow of materials through production lines and reducing downtime. In warehousing, precise tracking facilitates the effective implementation of strategies like First-In, First-Out (FIFO) or First-Expired, First-Out (FEFO), which helps decrease spoilage and obsolescence. Quicker turnover ensures that capital is not locked in slow-moving or surplus stock, thereby boosting cash flow and profitability.
Better Asset Security and Loss Prevention
RFID technology plays a crucial role in enhancing asset security and preventing loss or theft. High-value assets or sensitive materials can be tagged, and their movement can be monitored in real-time. Alerts can be triggered if an item leaves a designated area without authorization or deviates from its expected route. This proactive monitoring acts as a deterrent and allows for immediate action if a security breach occurs. Furthermore, accurate tracking reduces the chances of items being misplaced or lost within the warehouse, saving significant costs associated with replacement and operational disruptions. This improved security is a vital benefit for comprehensive warehousing and materials management.
Save Cost
Ultimately, the culmination of these benefits – improved accuracy, enhanced efficiency, real-time visibility, better utilization, and increased security – leads to substantial cost savings. Labor costs are reduced through the automation of data capture and streamlined processes. Losses due to errors, theft, damage, and obsolescence are minimized. Optimized inventory levels mean lower holding costs and reduced capital tied up in stock. While there is an initial investment in RFID infrastructure, the long-term return on investment (ROI) from these operational improvements and cost reductions is often significant, making RFID warehouse management a financially sound strategy for businesses looking to gain a competitive edge.
Common RFID Tags Used in Efficient Warehousing and Materials Management
The effectiveness of an RFID warehouse management system heavily relies on selecting the appropriate RFID tags for the specific items and environmental conditions. Different tags offer varying read ranges, durability, attachment methods, and suitability for different material types.
RFID Cable Tie Tags in Retail Warehousing and Materials Management
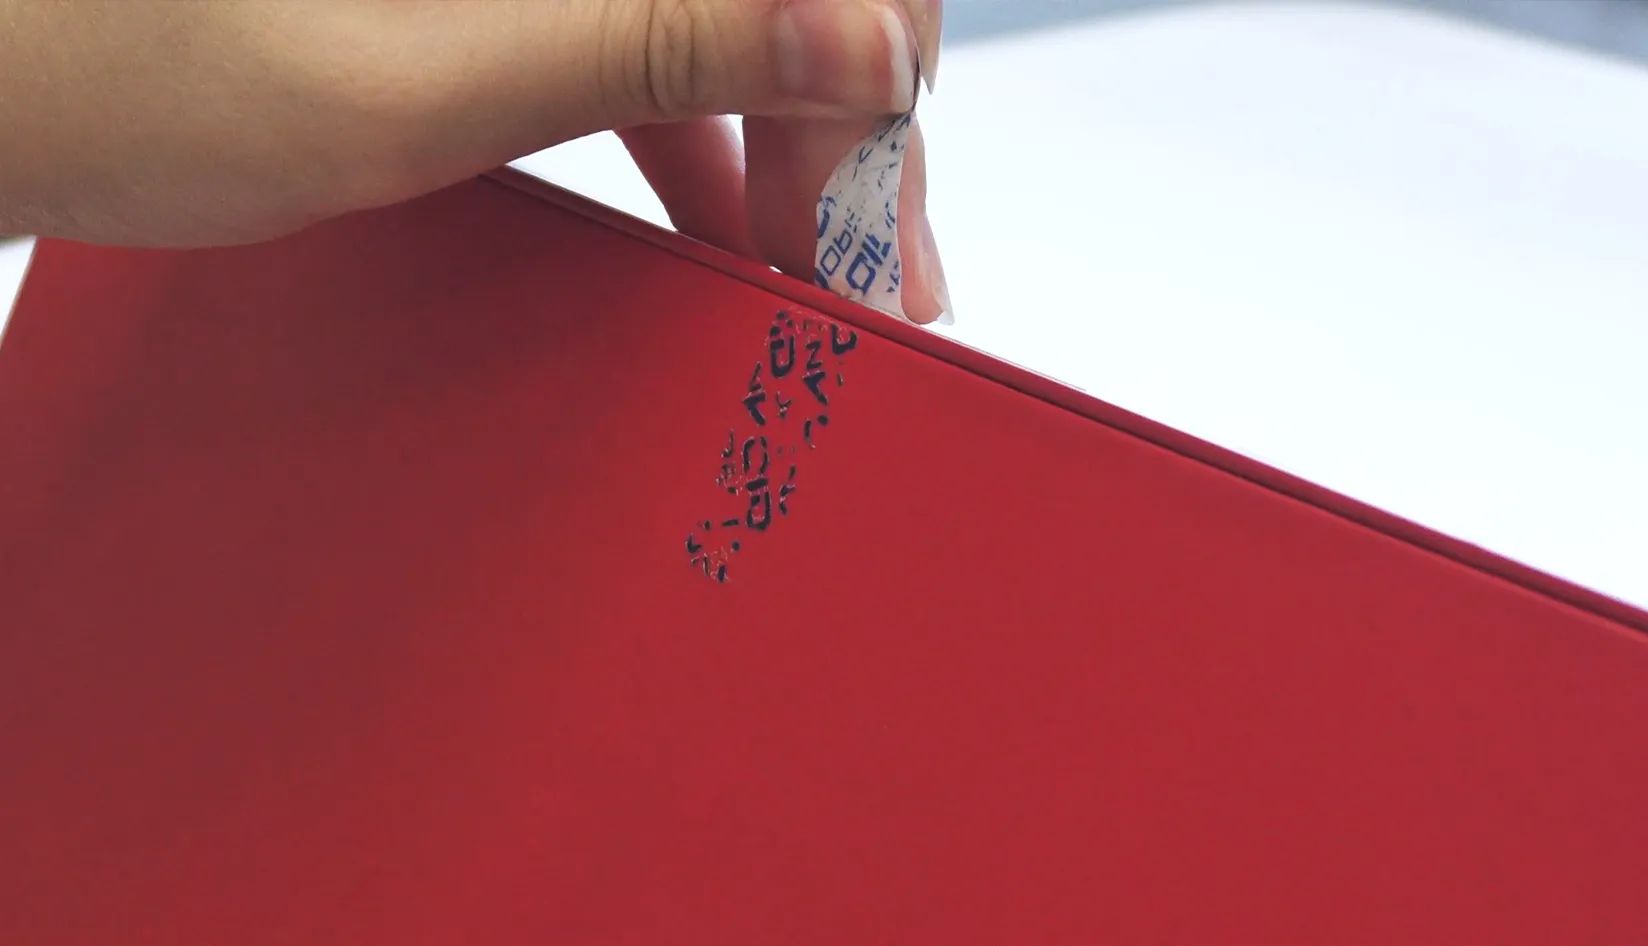
RFID cable tie tags offer a flexible solution for retail warehousing and materials management. These tags feature an RFID inlay within a durable nylon or plastic tie, allowing secure attachment to products, bundles, cages, or equipment. Their tamper-evident design is ideal for tracking valuable goods. In retail, they are essential for monitoring high-value electronics from distribution centers to sales floors, improving inventory visibility and reducing losses. Their easy application and removal make them versatile for dynamic warehouses, enhancing RFID efficiency in logistics by simplifying the tagging process.
RFID On-Metal Tags in Manufacturing and Construction
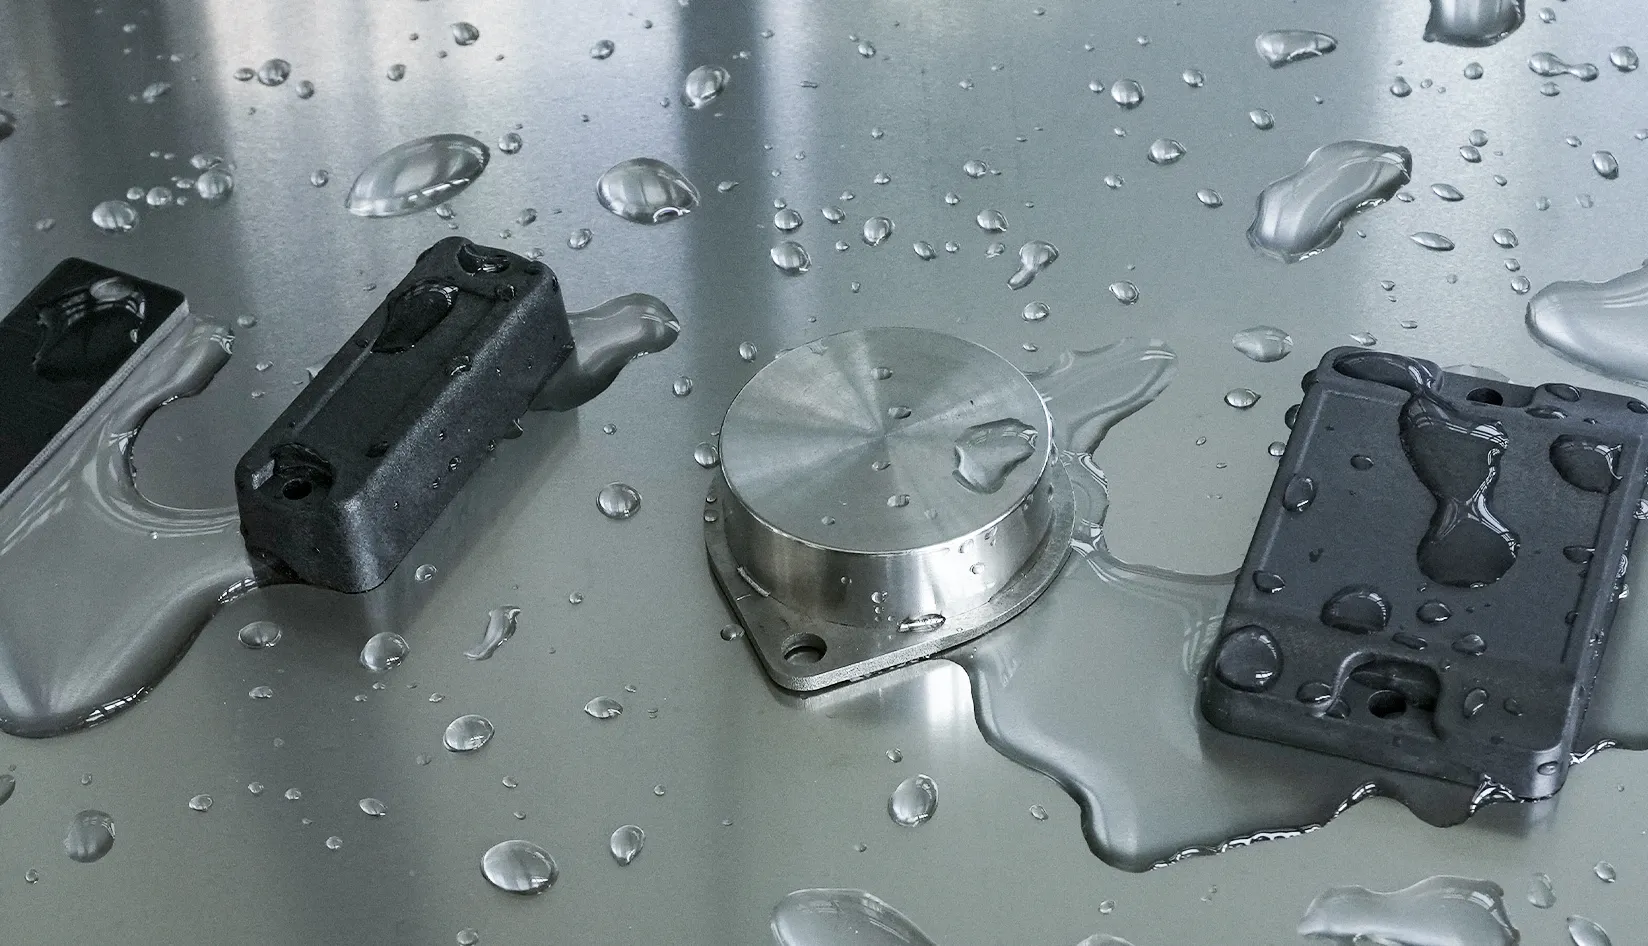
Monitoring assets in manufacturing and construction poses challenges due to metal surfaces and harsh conditions. Conventional RFID tags often fail on metal, as the material interferes with the antenna and absorbs radio frequencies, limiting read range. On-metal RFID tags address this by using a spacer or shielding layer to separate the RFID inlay from the metal, enabling effective signal transmission. These tags are designed to endure extreme temperatures, moisture, chemicals, and physical impacts. In manufacturing, they track tools, equipment, and products, while in construction, they manage equipment and monitor structural components. Accurate tracking of metallic assets is essential for optimizing RFID supply chains and ensuring efficient warehousing and asset management.
Real-World Industry Case Studies of RFID in Retail Warehousing and Materials Management
Across various industries, businesses are successfully implementing RFID warehouse management solutions to overcome longstanding challenges and gain a competitive edge.
UNIQLO’s RFID Storage Management
Fast Retailing, the parent company of the global apparel brand UNIQLO, embarked on a large-scale RFID implementation to revolutionize its supply chain and in-store operations. Currently, the company has integrated RFID into its warehouse operations. Reports indicate that UNIQLO has equipped all its products with RFID tags, which work in conjunction with automated material handling systems. This transition to an automated warehouse has drastically cut down the workforce from approximately 100 employees to just 10, achieving a remarkable 90% reduction in labor costs. Additionally, UNIQLO has seen an astonishing 80-fold increase in production efficiency, a 19-fold boost in shipment productivity, a threefold enhancement in storage efficiency, an 80% decrease in personnel training expenses, and a flawless 100% accuracy rate in RFID automatic detection.

Eskimo Cold Storage RFID Inventory Tracking
Eskimo Cold Storage revolutionized its cold storage operations by implementing RFID inventory tracking at the pallet level, thanks to Datex Corporation’s Footprint 3PL WMS. Before adopting RFID technology, they struggled with inventory management, resulting in approximately 3% of their 139,000 annual pallet movements—over 4,000 pallets—being mishandled. Each lost pallet incurred a cost of about $50 in labor and time, culminating in an estimated annual loss of $208,000, in addition to $25,000 in chargebacks. However, with the introduction of RFID, they gained real-time visibility into their inventory, significantly reduced errors, and enhanced operational efficiency, achieving a remarkable return on investment in just four months.

Conclusion
Radio Frequency Identification (RFID) technology presents a compelling and effective solution for dramatically improving warehousing and materials management. By transcending the constraints of manual methods and conventional barcode systems, RFID empowers businesses to attain unmatched levels of inventory precision, operational effectiveness, and real-time visibility. The capacity to automate data collection, monitor goods effortlessly, and minimize human error leads to significant cost reductions, enhanced asset security, and better material utilization. As the journey towards digital transformation in logistics continues, RFID emerges as a vital catalyst. Now is the perfect time to embrace RFID for a more efficient and agile supply chain.
FAQs
Is RFID suitable for small warehouses or businesses?
Yes, RFID can be highly beneficial for small warehouses and businesses, not just large enterprises. Although the upfront cost may raise concerns, scalable RFID solutions are designed to accommodate different business needs. The improvements in inventory accuracy, labor efficiency, and error reduction can offer a significant return on investment even for smaller operations.
Can RFID tags be reused in warehousing and material management?
Absolutely. Many RFID tags, especially those designed for tracking assets like pallets, containers, or tools, are built for durability and can be reused multiple times. This reusability is a key factor in the cost-effectiveness of an RFID in the logistics system.
Is RFID data secure? Can it support encryption or password protection?
Many RFID chips support encryption of the data stored on the tag. Access to tag data can also support password protection, preventing unauthorized reading or modification.
What industries benefit the most from RFID in warehouse management?
A wide range of industries can benefit significantly from RFID warehouse management. Retail and apparel (like UNIQLO) gain from improved inventory accuracy and loss prevention. Manufacturing uses RFID for tracking work-in-progress and tools. Pharmaceuticals and healthcare rely on it for tracking high-value drugs and medical equipment, ensuring compliance and patient safety. Logistics and transportation providers use RFID for asset tracking and improving shipment visibility. Agriculture and food industries, including cold chain logistics (like Eskimo Cold Storage), use RFID for traceability and managing perishable goods.


 EN
 ES
 JA